Choosing 3d printing technology is not a contest to find the newest machine. It is a business decision about parts, production volume, materials, and the work your team can reliably support. A prototype that fits on a desk has different needs from a replacement component exposed to heat or repeated stress. The details matter.
Dr. Joseph DeSimone, co-founder of Carbon and a researcher in advanced manufacturing, has said, “3D printing is actually a misnomer.” His point is a useful reminder: the label covers processes with very different strengths. Fused deposition modeling can suit affordable prototypes and functional parts; resin printing can capture fine detail; powder-bed systems can produce complex geometries without the same support structures. Metal processes bring other considerations, including equipment, post-processing, and operator expertise.
There is no universal winner. Start with the part you need to make, then consider tolerances, material performance, surface finish, throughput, and total cost—not just the printer’s purchase price. Picture a bracket that must fit an existing assembly: a small dimensional error may matter more than a flawless surface. Ask what happens after printing, too. Parts may need cleaning, curing, machining, or inspection.
A checklist helps. Real production is messier. A technology that looks ideal on paper may strain a small team’s time or budget. The sections ahead compare common processes and explain how to test them against practical business requirements. The goal is not certainty. It is a defensible choice, backed by sample parts, supplier discussions, and honest limits.
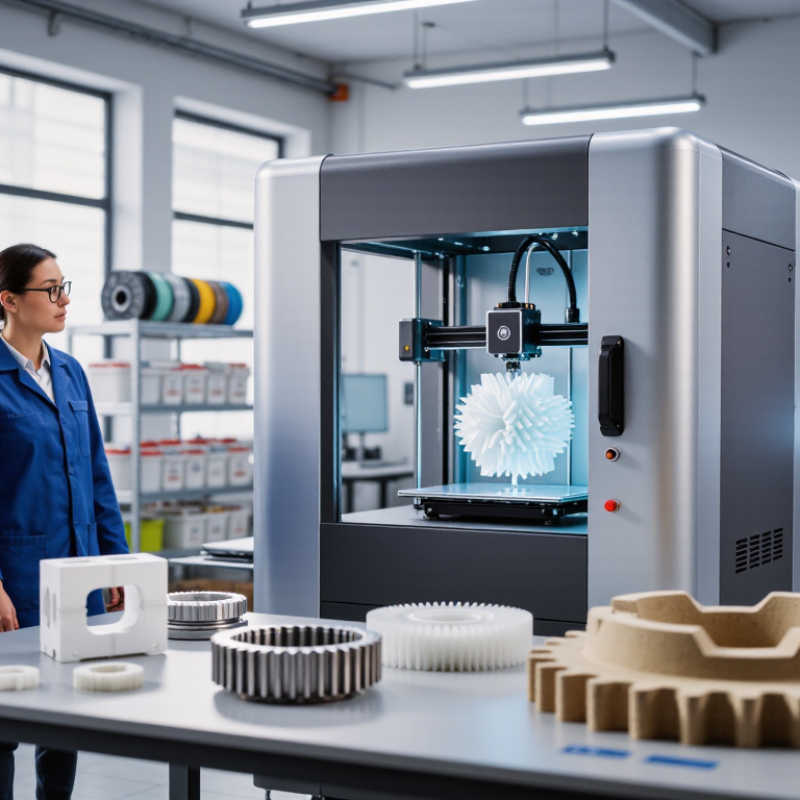
Before choosing a 3D printing process, describe the work your business actually needs done. Estimate parts per month, peak demand, and acceptable delivery times. Record each part’s dimensions, required fit, material exposure, and visible surface areas. A small bracket used indoors has different needs from a large housing exposed to heat. Be specific. “High quality” is not a useful measurement; a tolerance range or sample part is better.
Tips: Gather three representative parts and note their size, function, and current production cost. Include failed prints and rework. They reveal requirements that spreadsheets may miss.
Separate prototypes from repeat production. Prototypes may prioritize quick changes, while regular orders need consistent dimensions and predictable labor. Track how much time goes into support removal, sanding, inspection, and assembly. Those tasks can change the real cost. Also ask whether parts must match across separate production runs. A few successful samples do not prove long-term consistency. Estimates will be imperfect at first; revise them after a small trial run, and document what changed.
Fused deposition modeling works well for affordable fit checks, brackets, and larger parts. It deposits melted filament in visible layers, so surfaces may need sanding. Material choices and part strength vary, and thin features can be unreliable. A quick print can still reveal a poor design.
Stereolithography cures liquid resin with light, producing fine details and smooth surfaces. It suits small housings, intricate models, and parts where appearance matters. However, supports need removal, and some resins can be brittle or require careful post-curing. A glossy finish is not proof of durability. Not always.
Selective laser sintering fuses polymer powder, often producing durable parts without separate support structures. That makes it useful for complex shapes and small production runs. The surface is usually grainier than a resin print, and powder handling adds process steps. Metal powder bed fusion can create strong, complex metal components, but equipment, finishing, and inspection needs are substantial.
Compare technologies using the actual part, not a generic sample. Check dimensions, load direction, operating temperature, finish, and expected quantity. Request a test piece with a thin wall or tight hole, then measure it. One practical limitation: published capability ranges may not match your material, machine settings, or supplier’s workflow. A small trial can expose that mismatch before it becomes an expensive assumption.
Compare typical layer-thickness ranges across common 3D printing technologies. Thinner layers can capture finer vertical detail, but do not alone determine overall part accuracy or print quality.
Ranges are representative industry values; actual settings vary by machine, material, and application. Lower layer thickness may increase printing time.
Choosing a printing technology starts with the part’s job, not a machine’s advertised resolution. List its expected loads, operating temperature, chemical exposure, and required surface finish. A clip near a warm motor needs different material behavior from a display model. Write these conditions down. This small step can prevent a detailed prototype from failing in use.
Fused-filament printing works well for functional parts made from common thermoplastics, especially when size and affordability matter. Layer direction matters. A bracket loaded across its layers may split sooner than one loaded along them. Resin-based printing captures tiny lettering and smooth contours, but some resins can be brittle or sensitive to sunlight. Powder-bed printing suits interlocking shapes and complex internal channels because surrounding powder supports the part. Its surface may feel grainy, though, and cleanup takes time.
Match the design to the process before finalizing wall thickness, holes, and supports. Thin walls can warp; narrow channels may trap powder or resin. Metal powder-bed processes can produce strong, intricate components, but they usually require careful orientation and post-processing. One early design choice may still prove wrong. Print a small test section, measure critical features, and check how the actual material behaves under realistic conditions. A datasheet helps, but it cannot replace testing the finished part.
Choosing a 3D printing process starts with the part, not the machine. List the required materials, dimensions, tolerances, surface finish, and monthly volume. A bracket hidden inside equipment may tolerate rougher surfaces than a visible product enclosure. Filament processes can suit larger functional prototypes, while resin processes often capture finer detail. Powder-based processes can produce complex geometries, but they need careful powder handling and post-processing. Inspect sample parts; specification sheets may not reveal support marks or warping.
Compare the full workflow, not just the purchase price. Include installation, ventilation, materials, labor, maintenance, failed prints, and finishing tools. A low-cost machine can become expensive if every part needs lengthy cleanup. Ask who will prepare files, monitor jobs, and troubleshoot failed builds. A spreadsheet helps, but it can miss downtime and staff learning time. Run a small pilot using representative parts before committing. Record print duration, usable yield, and hands-on minutes per part. The result may challenge your first estimate.
Tips: Map each step from design file to finished part. Confirm available space, power, safety controls, and staff capacity. Leave room for imperfect prints; they happen.
| Technology | Typical Equipment Cost (USD) | Suitable Materials | Workflow and Post-Processing | Operating Needs | Best-Fit Business Uses | Key Trade-Off |
|---|---|---|---|---|---|---|
| Fused Deposition Modeling (FDM) | About $300–$5,000 for many desktop systems; approximately $10,000–$100,000 or more for industrial systems. | Common thermoplastics such as PLA, PETG, ABS, and nylon; specialized systems may process higher-performance polymers. | Load filament, prepare the build, print, remove supports, and optionally sand or finish. Supports can add labor and material waste. | Generally straightforward to operate. Consider ventilation, a stable temperature, nozzle and bed maintenance, and dry storage for moisture-sensitive filament. | Low-cost prototypes, concept models, jigs, fixtures, and larger functional parts where surface finish is not the top priority. | Accessible equipment and materials, but visible layer lines and anisotropic strength may limit appearance or performance. |
| Vat Photopolymerization (SLA/DLP) | About $500–$5,000 for many desktop systems; approximately $10,000–$100,000 or more for production-oriented systems. | Liquid photopolymer resins, including general-purpose, flexible, castable, and engineering formulations. | Print, drain the part, remove supports, wash in solvent, and post-cure with light. Resin handling and waste disposal require care. | Plan for gloves, suitable ventilation, solvent storage, washing and curing equipment, and procedures for uncured resin and solvent waste. | Detailed prototypes, small components, dental or jewelry workflows, and models that need smooth surfaces and fine features. | High detail and smooth surfaces, but parts may be brittle or UV-sensitive, and the washing and curing steps add workflow time. |
| Selective Laser Sintering (SLS) | Roughly $20,000–$100,000 for some compact systems; industrial production systems can cost $100,000–$500,000 or more. | Powdered polymers, commonly nylon-based materials; available options depend on the system and process. | Prepare and pack the build, print, cool, unpack, remove loose powder, and optionally bead-blast or dye parts. Unfused powder may be reused within process limits. | Requires powder handling, dust control, regular cleaning, and space for unpacking and finishing. Build cooling can extend the production cycle. | Durable functional prototypes, complex geometries, small production runs, and parts that benefit from support-free nesting. | Can produce interlocking and complex parts without printed supports, but powder management and finishing increase operational demands. |
| Material Jetting | Often about $50,000–$200,000 or more, depending on build size, material capability, and configuration. | Photopolymer materials; some systems support multiple material properties or colors in one build. | Print droplets of material, remove support material, and clean parts. Some materials may require additional curing or careful handling. | Budget for material-specific storage, support removal, machine upkeep, and trained operators. Consumable costs can be significant. | High-detail visual prototypes, presentation models, and parts that need multiple colors or material properties. | Strong visual detail and multi-material capability, but equipment and consumables can be costly and parts may not suit demanding end-use conditions. |
| Metal Powder Bed Fusion | Typically several hundred thousand dollars to over $1 million for a complete industrial setup; ancillary equipment can add substantially to the investment. | Metal powders such as stainless steel, aluminum, titanium, and nickel-based alloys, subject to system compatibility. | Print in a controlled atmosphere, remove powder, detach parts from the build plate, and often perform heat treatment and machining. | Requires specialized facilities, powder safety controls, inert-gas or atmosphere management, trained staff, and robust quality procedures. | Complex metal components, lightweight structures, high-value parts, and applications where conventional manufacturing is difficult. | Enables complex metal geometries, but has high capital, safety, qualification, and post-processing requirements. |
Cost and planning note: Equipment figures are broad indicative purchase-price ranges in USD, not quotes. Actual costs vary with build volume, material capability, automation, region, service contracts, installation, facility upgrades, and post-processing equipment. Compare total cost per usable part—including materials, labor, maintenance, rejects, finishing, and machine utilization—not just the printer price.
A technology may produce an impressive sample and still fail your daily workflow. Validate your choice with a pilot project that uses a representative part, not a decorative demo. Include the thin walls, tight fits, or awkward supports your real products require. Keep the test small. Keep it realistic.
Track more than print time. Record material use, setup effort, failed builds, finishing time, and dimensional accuracy. Ask an operator to handle the part, then check whether it fits as intended. A spreadsheet helps, but notes beside the machine can reveal delays that numbers miss. Small details count.
A pilot can mislead you if it tests only one easy part or relies on an unusually experienced operator. Try more than one build, and use the same acceptance criteria each time. Compare results with your actual production needs, including repeatability and post-processing labor. Some findings may be inconvenient. That is useful. If the process needs constant adjustment, or finishing erases its speed advantage, record that plainly. The best choice is not always the one with the cleanest sample; it is the one your team can use reliably.

© Copyrights Levil Technology Corp 2022